Lockout and Tagout Programmes and Placards
Hazardous energy control is among the most frequently cited findings in Ontario industrial inspections, and among the most consequential when it fails. The failure is rarely an absence of locks. It is usually an absence of machine-specific procedure: workers hold the hardware but have no written instruction telling them which energy sources exist on a particular machine, in what order to isolate them, and how to verify that isolation has been achieved.
PHASCORP develops hazardous energy control programmes, writes machine-specific isolation procedures, produces the placards that sit on the equipment itself, and trains the workers who use them.
Request a scoping call: (647) 564-6824
The regulatory position
Regulation 851, the Industrial Establishments regulation, governs this in Ontario. It requires that where a part of a machine may endanger a worker, cleaning, oiling, adjusting, repairing or maintenance be carried out only when motion that may endanger the worker has stopped, and that the machine be locked out and blocked where required to prevent movement.
CSA Z460, the standard for the control of hazardous energy, is the benchmark against which inspectors and auditors generally evaluate a programme. It is recognised practice rather than law in Ontario, but a programme departing materially from it is difficult to defend.
The energy sources a complete programme must address extend beyond electrical isolation to hydraulic and pneumatic pressure, stored mechanical energy in springs and counterweights, gravity, thermal energy and residual chemical energy.
Machine-specific placards
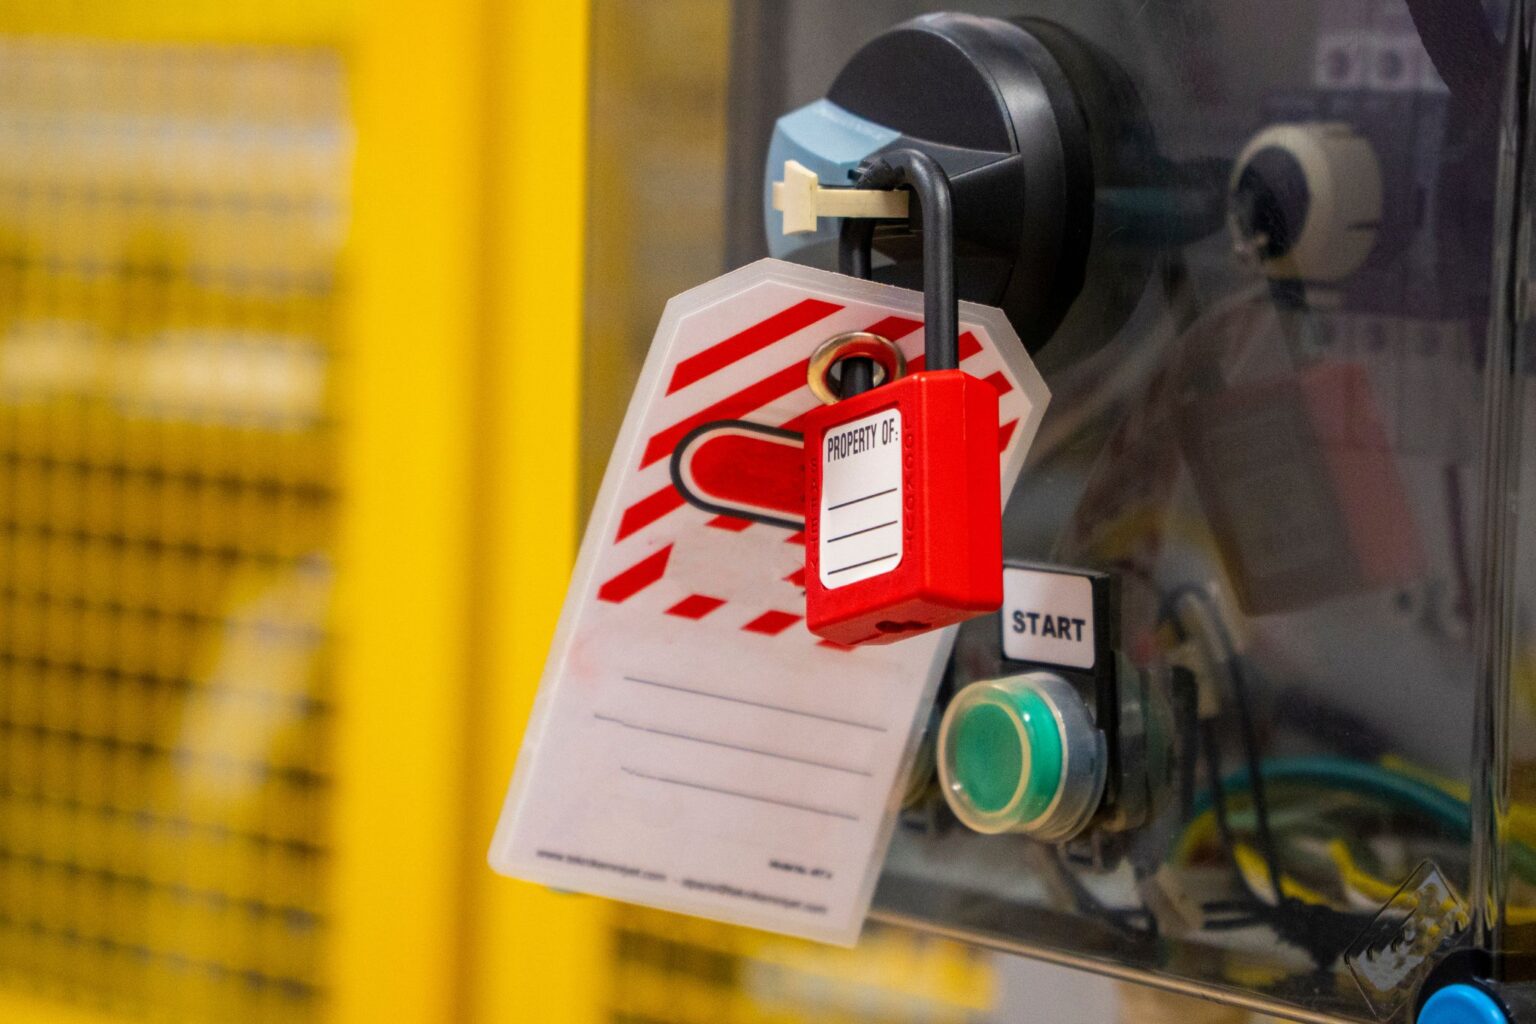
A general lockout procedure is a policy. A machine-specific placard is an instruction.
We develop placards for each piece of equipment in a facility, identifying the energy sources present on that machine, their isolation points, the correct sequence of isolation, the means of dissipating stored energy, and the verification step. The placard is mounted on or adjacent to the equipment, so that the instruction is present at the point and moment of use rather
than filed in an office.
This is the single most effective intervention available in this area. It converts an abstract requirement into a specific and followable set of steps, and it substantially reduces the scope for error where a worker is servicing equipment they do not operate daily.
What a complete programme includes
A written hazardous energy control programme setting out scope, responsibilities and procedure. An energy source survey of the equipment in the facility. Machine-specific isolation procedures and placards. Lock and tag hardware standards and accountability for their issue. Group lockout procedure, which is where multi-trade maintenance work most often goes wrong. Shift handover provisions. Contractor lockout requirements. Periodic verification that the programme is being followed. Training for authorised, affected and other workers, differentiated by role.
Training
Not everyone requires the same instruction. Authorised workers who perform isolation need procedural training and practical verification. Affected workers who operate the equipment need to recognise a lockout in progress and understand that they must not attempt to restore energy. Supervisors need to understand group lockout, shift handover and contractor control.
We deliver this training and, where a programme is being introduced or substantially revised, we prefer to deliver it after the placards are in place, so that workers are trained on the actual procedures they will use rather than on a general description of them.
The connection to machine guarding
Hazardous energy control and machine guarding are assessed together in practice, because they address the same underlying hazard from two directions. Guarding prevents contact during normal operation; lockout prevents energisation during service. A facility strong in one and weak in the other is not protected.
Cost
Quoted according to the number of machines requiring an energy source survey and placard development, the number of sites, and whether training and programme documentation are included.
Request a scoping call: (647) 564-6824 or info@phascorp.com
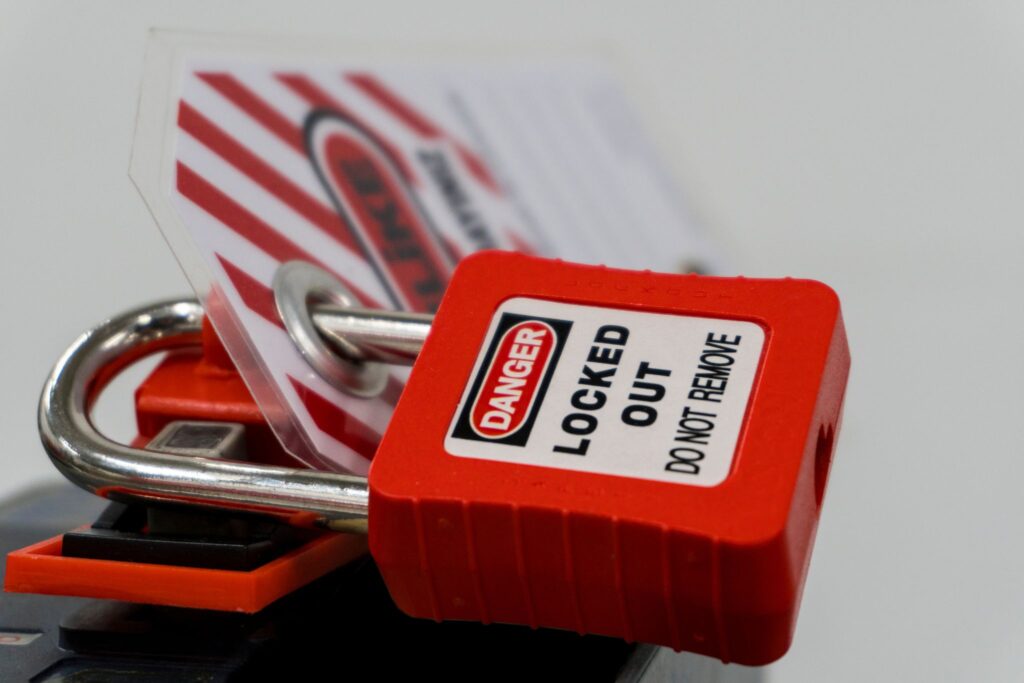
A documented system for controlling hazardous energy so that machinery cannot be energised or move unexpectedly while a worker is servicing it. It comprises a written programme, machine specific isolation procedures, hardware standards, training and periodic verification.
Regulation 851 requires that cleaning, oiling, adjusting, repairing and maintenance be performed only when motion that may endanger a worker has stopped, and that machinery be locked out and blocked as required. CSA Z460, the standard for the control of hazardous energy, is the benchmark against which programmes are generally evaluated.
Machine-specific instruction cards mounted on or beside a piece of equipment, identifying the energy sources present, the isolation points, the correct sequence, the means of dissipating stored energy and the verification step. They place the procedure at the point of use rather than in a binder.
Electrical, hydraulic, pneumatic, stored mechanical energy including springs and counterweights, gravity, thermal and residual chemical energy. Programmes addressing electrical isolation alone are incomplete and this is a common audit finding.
Authorised workers who perform isolation require procedural training and practical verification. Affected workers who operate the equipment require training in recognising a lockout and in not attempting to restore energy. Supervisors additionally require training in group lockout, shift handover and contractor control.
The procedure applied where several workers, often from different trades, are servicing the same equipment simultaneously. Each worker must have individual protection that cannot be removed by another. Group lockout is where multi-trade maintenance most frequently fails.
Contractors performing work on your equipment must be subject to a defined lockout arrangement, whether that is your procedure, theirs, or a documented reconciliation of the two. Undefined contractor lockout is a recurring finding in industrial audits.
Yes. We conduct an energy source survey of the equipment and develop a placard for each machine, which is generally the most effective single measure available in this area.